Free printable chart
Tap drill chart
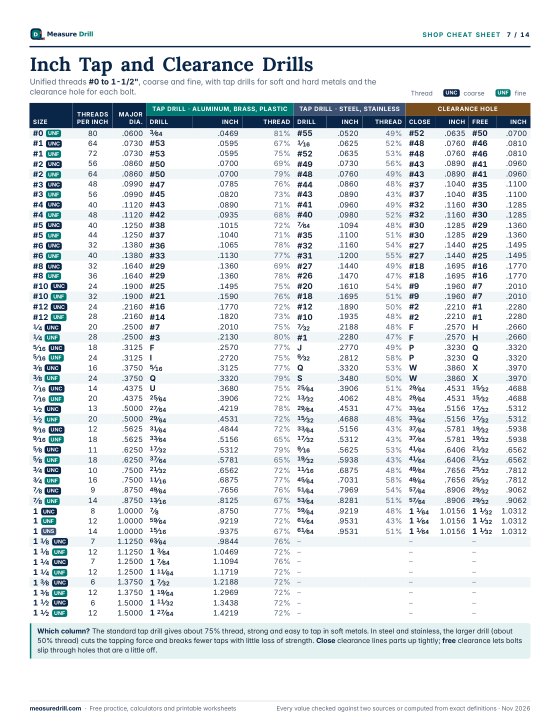
The drill to use before tapping every common inch, metric and pipe thread, plus the clearance hole each bolt slips through.
Prints on two US Letter pages · Free for home, shop and classroom use · Every value checked
Tap drill chart
Inch threads, UNC and UNF
Tap drill gives about 75% thread for aluminum, brass and plastic. The steel drill gives about 50% thread for tough metals. Close and free are clearance holes.
| Thread | TPI | Tap drill | Inch | Thread | Steel drill | Close | Free |
|---|---|---|---|---|---|---|---|
| #0-80 UNF | 80 | 3⁄64 | .0469 | 81% | #55 | #52 | #50 |
| #1-64 UNC | 64 | #53 | .0595 | 67% | 1⁄16 | #48 | #46 |
| #1-72 UNF | 72 | #53 | .0595 | 75% | #52 | #48 | #46 |
| #2-56 UNC | 56 | #50 | .0700 | 69% | #49 | #43 | #41 |
| #2-64 UNF | 64 | #50 | .0700 | 79% | #48 | #43 | #41 |
| #3-48 UNC | 48 | #47 | .0785 | 76% | #44 | #37 | #35 |
| #3-56 UNF | 56 | #45 | .0820 | 73% | #43 | #37 | #35 |
| #4-40 UNC | 40 | #43 | .0890 | 71% | #41 | #32 | #30 |
| #4-48 UNF | 48 | #42 | .0935 | 68% | #40 | #32 | #30 |
| #5-40 UNC | 40 | #38 | .1015 | 72% | 7⁄64 | #30 | #29 |
| #5-44 UNF | 44 | #37 | .1040 | 71% | #35 | #30 | #29 |
| #6-32 UNC | 32 | #36 | .1065 | 78% | #32 | #27 | #25 |
| #6-40 UNF | 40 | #33 | .1130 | 77% | #31 | #27 | #25 |
| #8-32 UNC | 32 | #29 | .1360 | 69% | #27 | #18 | #16 |
| #8-36 UNF | 36 | #29 | .1360 | 78% | #26 | #18 | #16 |
| #10-24 UNC | 24 | #25 | .1495 | 75% | #20 | #9 | #7 |
| #10-32 UNF | 32 | #21 | .1590 | 76% | #18 | #9 | #7 |
| #12-24 UNC | 24 | #16 | .1770 | 72% | #12 | #2 | #1 |
| #12-28 UNF | 28 | #14 | .1820 | 73% | #10 | #2 | #1 |
| 1⁄4-20 UNC | 20 | #7 | .2010 | 75% | 7⁄32 | F | H |
| 1⁄4-28 UNF | 28 | #3 | .2130 | 80% | #1 | F | H |
| 5⁄16-18 UNC | 18 | F | .2570 | 77% | J | P | Q |
| 5⁄16-24 UNF | 24 | I | .2720 | 75% | 9⁄32 | P | Q |
| 3⁄8-16 UNC | 16 | 5⁄16 | .3125 | 77% | Q | W | X |
| 3⁄8-24 UNF | 24 | Q | .3320 | 79% | S | W | X |
| 7⁄16-14 UNC | 14 | U | .3680 | 75% | 25⁄64 | 29⁄64 | 15⁄32 |
| 7⁄16-20 UNF | 20 | 25⁄64 | .3906 | 72% | 13⁄32 | 29⁄64 | 15⁄32 |
| 1⁄2-13 UNC | 13 | 27⁄64 | .4219 | 78% | 29⁄64 | 33⁄64 | 17⁄32 |
| 1⁄2-20 UNF | 20 | 29⁄64 | .4531 | 72% | 15⁄32 | 33⁄64 | 17⁄32 |
| 9⁄16-12 UNC | 12 | 31⁄64 | .4844 | 72% | 33⁄64 | 37⁄64 | 19⁄32 |
| 9⁄16-18 UNF | 18 | 33⁄64 | .5156 | 65% | 17⁄32 | 37⁄64 | 19⁄32 |
| 5⁄8-11 UNC | 11 | 17⁄32 | .5312 | 79% | 9⁄16 | 41⁄64 | 21⁄32 |
| 5⁄8-18 UNF | 18 | 37⁄64 | .5781 | 65% | 19⁄32 | 41⁄64 | 21⁄32 |
| 3⁄4-10 UNC | 10 | 21⁄32 | .6562 | 72% | 11⁄16 | 49⁄64 | 25⁄32 |
| 3⁄4-16 UNF | 16 | 11⁄16 | .6875 | 77% | 45⁄64 | 49⁄64 | 25⁄32 |
| 7⁄8-9 UNC | 9 | 49⁄64 | .7656 | 76% | 51⁄64 | 57⁄64 | 29⁄32 |
| 7⁄8-14 UNF | 14 | 13⁄16 | .8125 | 67% | 53⁄64 | 57⁄64 | 29⁄32 |
| 1-8 UNC | 8 | 7⁄8 | .8750 | 77% | 59⁄64 | 1 1⁄64 | 1 1⁄32 |
| 1-12 UNF | 12 | 59⁄64 | .9219 | 72% | 61⁄64 | 1 1⁄64 | 1 1⁄32 |
| 1-14 UNS | 14 | 15⁄16 | .9375 | 67% | 61⁄64 | 1 1⁄64 | 1 1⁄32 |
| 1 1⁄8-7 UNC | 7 | 63⁄64 | .9844 | 76% | – | – | – |
| 1 1⁄8-12 UNF | 12 | 1 3⁄64 | 1.0469 | 72% | – | – | – |
| 1 1⁄4-7 UNC | 7 | 1 7⁄64 | 1.1094 | 76% | – | – | – |
| 1 1⁄4-12 UNF | 12 | 1 11⁄64 | 1.1719 | 72% | – | – | – |
| 1 3⁄8-6 UNC | 6 | 1 7⁄32 | 1.2188 | 72% | – | – | – |
| 1 3⁄8-12 UNF | 12 | 1 19⁄64 | 1.2969 | 72% | – | – | – |
| 1 1⁄2-6 UNC | 6 | 1 11⁄32 | 1.3438 | 72% | – | – | – |
| 1 1⁄2-12 UNF | 12 | 1 27⁄64 | 1.4219 | 72% | – | – | – |
Metric threads
Tap drill = size − pitch. The closest inch drill is within 0.008". Clearance holes in mm follow ISO 273.
| Thread | Tap drill | Inch | Closest inch drill | Close mm | Normal mm | Loose mm |
|---|---|---|---|---|---|---|
| M1.6 x 0.35 coarse | 1.25 mm | .0492 | 3⁄64 | 1.7 | 1.8 | 2 |
| M2 x 0.4 coarse | 1.6 mm | .0630 | 1⁄16 | 2.2 | 2.4 | 2.6 |
| M2.5 x 0.45 coarse | 2.05 mm | .0807 | #46 | 2.7 | 2.9 | 3.1 |
| M3 x 0.5 coarse | 2.5 mm | .0984 | #40 | 3.2 | 3.4 | 3.6 |
| M3.5 x 0.6 coarse | 2.9 mm | .1142 | #33 | 3.7 | 3.9 | 4.2 |
| M4 x 0.7 coarse | 3.3 mm | .1299 | #30 | 4.3 | 4.5 | 4.8 |
| M5 x 0.8 coarse | 4.2 mm | .1654 | #19 | 5.3 | 5.5 | 5.8 |
| M6 x 1 coarse | 5 mm | .1969 | #9 | 6.4 | 6.6 | 7 |
| M8 x 1.25 coarse | 6.8 mm | .2677 | H | 8.4 | 9 | 10 |
| M8 x 1 fine | 7 mm | .2756 | J | 8.4 | 9 | 10 |
| M10 x 1.5 coarse | 8.5 mm | .3346 | Q | 10.5 | 11 | 12 |
| M10 x 1.25 fine | 8.8 mm | .3465 | S | 10.5 | 11 | 12 |
| M10 x 1 fine | 9 mm | .3543 | T | 10.5 | 11 | 12 |
| M12 x 1.75 coarse | 10.2 mm | .4016 | Y | 13 | 13.5 | 14.5 |
| M12 x 1.5 fine | 10.5 mm | .4134 | Z | 13 | 13.5 | 14.5 |
| M12 x 1.25 fine | 10.8 mm | .4252 | 27⁄64 | 13 | 13.5 | 14.5 |
| M14 x 2 coarse | 12 mm | .4724 | 15⁄32 | 15 | 15.5 | 16.5 |
| M14 x 1.5 fine | 12.5 mm | .4921 | 31⁄64 | 15 | 15.5 | 16.5 |
| M16 x 2 coarse | 14 mm | .5512 | 35⁄64 | 17 | 17.5 | 18.5 |
| M16 x 1.5 fine | 14.5 mm | .5709 | 37⁄64 | 17 | 17.5 | 18.5 |
| M18 x 2.5 coarse | 15.5 mm | .6102 | 39⁄64 | 19 | 20 | 21 |
| M18 x 1.5 fine | 16.5 mm | .6496 | 21⁄32 | 19 | 20 | 21 |
| M20 x 2.5 coarse | 17.5 mm | .6890 | 11⁄16 | 21 | 22 | 24 |
| M20 x 1.5 fine | 18.5 mm | .7283 | 47⁄64 | 21 | 22 | 24 |
| M22 x 2.5 coarse | 19.5 mm | .7677 | 49⁄64 | 23 | 24 | 26 |
| M22 x 1.5 fine | 20.5 mm | .8071 | 13⁄16 | 23 | 24 | 26 |
| M24 x 3 coarse | 21 mm | .8268 | 53⁄64 | 25 | 26 | 28 |
| M24 x 2 fine | 22 mm | .8661 | 55⁄64 | 25 | 26 | 28 |
| M27 x 3 coarse | 24 mm | .9449 | 15⁄16 | 28 | 30 | 32 |
| M30 x 3.5 coarse | 26.5 mm | 1.0433 | 1 3⁄64 | 31 | 33 | 35 |
Pipe threads, NPT
Drill sizes for tapping without a reamer (ANSI Dryseal recommendations). If you ream first, drill one size smaller. Match pipe size by the outside diameter.
| Pipe size | TPI | Tap drill | Inch | mm | Pipe OD (in) |
|---|---|---|---|---|---|
| 1⁄16" NPT | 27 | C | .2420 | 6.15 | .312 |
| 1⁄8" NPT | 27 | Q | .3320 | 8.43 | .405 |
| 1⁄4" NPT | 18 | 7⁄16 | .4375 | 11.11 | .540 |
| 3⁄8" NPT | 18 | 9⁄16 | .5625 | 14.29 | .675 |
| 1⁄2" NPT | 14 | 45⁄64 | .7031 | 17.86 | .840 |
| 3⁄4" NPT | 14 | 29⁄32 | .9062 | 23.02 | 1.050 |
| 1" NPT | 11.5 | 1 9⁄64 | 1.1406 | 28.97 | 1.315 |
| 1 1⁄4" NPT | 11.5 | 1 31⁄64 | 1.4844 | 37.70 | 1.660 |
| 1 1⁄2" NPT | 11.5 | 1 23⁄32 | 1.7188 | 43.66 | 1.900 |
| 2" NPT | 11.5 | 2 3⁄16 | 2.1875 | 55.56 | 2.375 |
Questions
What size drill for a 1/4-20 tap?
Use a #7 drill (0.201"). It gives about 75% thread. In stainless or tough steel, a 7/32 drill (0.2188") cuts tapping effort with little loss of strength.
What size drill for an M8 tap?
For M8 x 1.25, use a 6.8 mm drill. The rule for metric threads is size minus pitch: 8 − 1.25 = 6.75, rounded to the stock 6.8 mm drill.
What is the tap drill formula?
For inch threads: drill = major diameter − 1 ÷ threads per inch. For metric threads: drill = size − pitch. Both give roughly 75% thread.
What is a clearance hole?
The hole a bolt passes through without threads. A close fit lines parts up accurately; a free or loose fit lets the bolt pass even if the holes are slightly off.
What size drill for a 1/2 NPT tap?
About 45/64" when tapping without a reamer. Pipe sizes are not the thread diameter: a 1/2" NPT thread is about 0.840" across.
More free charts
Sources
Measure Drill checks every number against these references or works it out from the exact definitions of the units.
- Machinery's Handbook (Industrial Press), drill, thread and fastener tables
- NIST Special Publication 811, Appendix B: Conversion factors